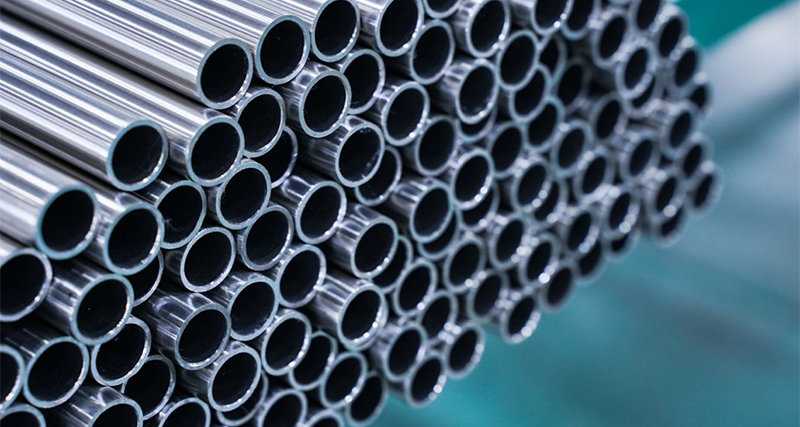
**Ultra High Purity Stainless Steel Tubing: Revolutionizing Industrial Applications**In the constantly evolving landscape of industrial manufacturing and processing, the demand for materials that combine superior quality, durability, and precision has never been higher. Among these materials, ultra high purity stainless steel tubing stands out as a critical component across a multitude of sectors, including semiconductors, pharmaceuticals, chemical processing, and food and beverage production. Recent developments in ultra high purity stainless steel tubing are set to redefine industry standards, offering enhanced performance and reliability that meet the stringent requirements of these high-tech fields.Ultra high purity stainless steel tubing is distinguished by its exceptional cleanliness and corrosion resistance, attributes that are vital for applications where contamination must be minimized and the integrity of the material preserved over time. Unlike conventional stainless steel products, ultra high purity tubing undergoes rigorous manufacturing processes designed to eliminate impurities and micro-defects that could compromise its performance in demanding environments.One of the key advancements in this field is the adoption of advanced metallurgical techniques and precision fabrication methods that significantly reduce the presence of inclusions and surface imperfections. These improvements ensure that the tubing maintains a uniform microstructure and smooth internal surfaces, which are essential for preventing particle generation and ensuring laminar flow of fluids or gases. This level of quality control is especially important in the semiconductor industry, where even microscopic contaminants can lead to costly defects and production downtime.Furthermore, the enhanced corrosion resistance of ultra high purity stainless steel tubing extends the service life of equipment, reducing maintenance needs and operational costs. Materials of this caliber are capable of withstanding aggressive chemical environments, high temperatures, and repeated sterilization cycles without degradation, making them ideal for pharmaceutical and biotechnological applications where sterility and durability are paramount.Recent innovations also include the integration of surface treatments and cleaning protocols that further elevate the tubing’s purity levels. Electropolishing and passivation techniques, for instance, are employed to create an ultra-smooth and chemically stable surface finish that prevents particle adhesion and microbial growth. These processes not only enhance the tubing's performance but also facilitate compliance with strict regulatory standards such as those imposed by the FDA and ISO for medical and food-grade applications.The global market for ultra high purity stainless steel tubing is witnessing rapid growth, driven by escalating investments in advanced manufacturing technologies and the expansion of end-use industries. Companies operating in this sector are increasingly focusing on customization and the development of tubing solutions tailored to the specific needs of their clients. This customer-centric approach includes offering a wide range of tubing dimensions, wall thicknesses, and alloy compositions to meet diverse operational requirements.Moreover, the emphasis on sustainable manufacturing practices is influencing the production of ultra high purity stainless steel tubing. Manufacturers are adopting environmentally friendly processes that minimize waste, reduce energy consumption, and promote the recyclability of materials. This commitment to sustainability aligns with the broader industrial trend towards greener operations and corporate responsibility.The versatility of ultra high purity stainless steel tubing is evident in its broad application spectrum. In the semiconductor industry, the tubing is used in ultra-high vacuum systems and gas delivery lines where contamination control is critical. In pharmaceuticals and biotech, it enables the sterile transfer of liquids and gases, maintaining the purity of sensitive products. The food and beverage sector benefits from the tubing’s hygienic properties, which ensure product quality and safety throughout processing and packaging stages.Looking ahead, research and development efforts continue to focus on enhancing the mechanical properties and performance characteristics of ultra high purity stainless steel tubing. Innovations in alloy design and manufacturing technology promise to deliver tubing options with even greater strength, flexibility, and resistance to extreme environments. Additionally, the integration of smart sensor technologies within piping systems is emerging as a potential avenue for real-time monitoring and predictive maintenance, further elevating the operational reliability of installations using these high-grade materials.In conclusion, ultra high purity stainless steel tubing represents a cornerstone in the advancement of modern industrial processes. Its superior purity, corrosion resistance, and tailored manufacturing make it indispensable for sectors that demand uncompromising quality and reliability. As industries continue to push the boundaries of technology and efficiency, the role of ultra high purity stainless steel tubing will only become more vital, driving innovation and enabling the achievement of new milestones in manufacturing excellence.
Read More